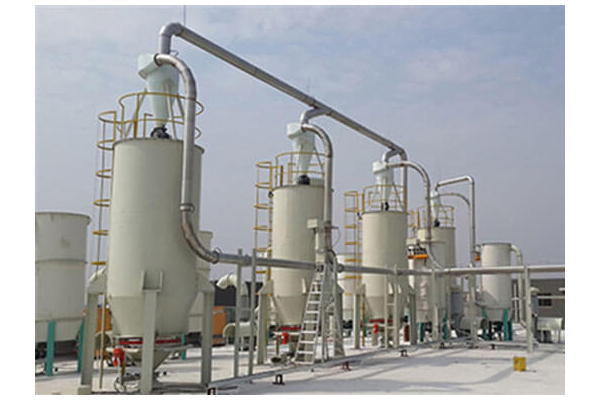
Precision Turnkey Projects is leading Pneumatic Conveying System Manufacturers in India. We are trusted Suppliers and Traders in India. A Pneumatic Conveying System is a modern material handling technology used for transporting powders, granules, and bulk materials through pipelines using air pressure.
With extensive industry experience, we provide Industrial Pneumatic Conveying Systems, Custom Pneumatic Conveying Systems, and Turnkey Pneumatic Conveying Solutions tailored to meet specific production requirements. Our product range includes Dense Phase Pneumatic Conveying Systems, Dilute Phase Pneumatic Conveying Systems, Vacuum Conveying Systems, Pressure Conveying Systems, Powder Conveying Systems, Bulk Material Conveying Systems, and Pneumatic Material Conveying Systems.
Every system is engineered using high-quality components and modern automation technology to ensure continuous material flow, low maintenance, reduced energy consumption, and maximum productivity. Our Automatic Pneumatic Conveying Systems are ideal for Bulk Solid Handling, Powder Transfer Systems, Food Grade Pneumatic Conveying, Chemical Powder Conveying, Plastic Granule Conveying, and other specialized industrial applications.
Top Pneumatic Conveying System Manufacturers in India specialize in designing and supplying efficient material handling solutions for the safe and reliable transportation of powders, granules, pellets, and other dry bulk materials. These systems use air pressure or vacuum to transfer materials through pipelines, offering benefits such as reduced material loss, improved hygiene, minimal manual handling, and efficient operation. Indian manufacturers provide customized pneumatic conveying systems, including dense-phase, dilute-phase, vacuum, and pressure conveying solutions, for industries such as pharmaceuticals, food processing, chemicals, plastics, cement, and other bulk-material handling applications.
A Pneumatic Conveying System is an automated transport system that uses air pressure or vacuum force to move dry bulk materials through enclosed pipelines. The system transfers materials from one processing point to another without manual handling.
These systems are commonly used for transporting powders, grains, pellets, chemicals, and other granular materials. By using controlled airflow, pneumatic conveyors provide smooth and efficient movement while maintaining material quality.
A pneumatic conveying system consists of major components such as blowers, vacuum pumps, pipelines, filters, separators, and receiving units. The system design depends on material characteristics, conveying distance, and production requirements.
The working principle of a Pneumatic Conveying System is based on the movement of materials using air velocity. A blower or vacuum pump generates airflow inside the conveying pipeline, creating the required force to transport materials.
The material enters the pipeline through a feeding mechanism, where it mixes with the moving air stream. The airflow carries the particles through the pipeline until they reach the destination point.
At the receiving end, separators or filters separate the transported material from the air. The material is collected in storage tanks, silos, or processing equipment, while clean air exits through filtration systems.
As we are leading Best Pneumatic Conveying System Manufacturers in India, our Types are designed to meet different application requirements and industry standards, including the following types:
As a leading Pneumatic Conveying System Manufacturers in India, we design and manufacture dilute phase and dense phase conveying systems engineered for efficient, dust-free, and continuous material handling across industries such as chemicals, plastics, food processing, cement, and pharmaceuticals.
| Specifications | Pneumatic Conveying System | Details |
|---|---|---|
| Working Principle | Pressure Differential Conveying | Bulk material moved through enclosed pipeline using compressed air/gas, created by blower, compressor, or vacuum pump |
| Conveying Method | Pressure / Vacuum / Combination | Pressure system pushes air from source (long distance, high throughput); Vacuum system pulls air from destination (short distance, multi-pickup); Combination for multi-source/multi-destination layouts |
| System Type | Dilute Phase / Dense Phase | Dilute phase: material suspended in high-velocity air (18-35 m/s), suited for long distance & lightweight material; Dense phase: low velocity slug flow (3-8 m/s), suited for fragile/abrasive material |
| Body Material | Mild Steel / Stainless Steel | MS for standard industrial use; SS 304/316 for food-grade & pharma applications; wear-resistant lined pipe for abrasive materials |
| Capacity | 1-2 tons/hr (customizable) | Scalable from a few kg/hr up to 30+ tons/hr depending on application |
| Conveying Distance | Up to 100 m (horizontal) / 30 m (vertical) | Industry range: 10-150+ meters horizontal, shorter for vertical runs |
| Material Handled | Powders, Granules, Pellets | Cement, fly ash, flour, sugar, spices, grains, PVC, resins, plastic pellets, pharmaceutical powders |
| Particle Size Suitability | Fine powder to small pellets | Typically up to a few mm; larger particle sizes possible with dense phase design |
| Input Voltage | 240 V / 415 V | As per motor rating and blower/compressor type selected |
| Motor Power | 1.3 kW (customizable) | Energy-efficient motor sized as per capacity & distance requirement |
| Air Pressure | Up to 10 bar | Dilute phase typically <1 bar (≤15 psig); Dense phase up to 2.5-6+ bar depending on design |
| Air Mover | Roots Blower / Screw Compressor / Vacuum Pump | Generates the pressure differential required for conveying |
| Feeder Type | Rotary Airlock / Venturi / Screw Feeder | Introduces material into the airstream at pickup point |
| Separation Unit | Cyclone Separator / Receiver | Separates conveyed material from air at the destination point |
| Filter Type | Bag Filter / Cartridge Filter | Captures fine dust before air exhaust for dust-free operation |
| Diverter Valves | Available (Optional) | Routes material to multiple discharge destinations |
| Frequency | 50 Hz | Standard for Indian industrial power supply |
| Automation Grade | Automatic (PLC/SCADA) | Fully automated monitoring & control of the entire conveying process |
| Surface Finishing | Polished / Powder Coated | Hygienic finish for food-grade and pharma pneumatic conveyor |
| Surface Treatment | Galvanized | Corrosion-resistant piping for industrial applications |
| Usage/Application | Industrial Material Handling | Cement plants, chemical industry, food processing, plastics, pharmaceuticals |
| Certification | ISO 9001:2015 Certified | Quality-assured manufacturing standards |
| Warranty | 1 Year (AMC available) | After-sales support & annual maintenance contract |
| Customization | Available | Turnkey pneumatic conveying system solutions as per client's material and process requirements |
As Pneumatic Conveying System Traders in India, our products provide several benefits including consistent quality, smooth finish, and long service life.
As Pneumatic Conveying System Manufacturers in India, our features ensure high precision, durability, and consistent performance.
As Pneumatic Conveying System Suppliers in India, our all types are used in various types of industrial sectors such as:
As one of the leading Pneumatic Conveying System Traders in India, we deliver premium-quality solutions designed to meet diverse industrial requirements. Here's why we stand out:
Choose Precision Turnkey Projects is leading Pneumatic Conveying System Manufacturers, Suppliers and Traders in India. A Pneumatic Conveying System is an efficient and reliable solution for transporting powders, grains, pellets, and bulk materials in modern industries. By using controlled airflow technology, these systems provide safe, hygienic, and automated material handling. From industrial pneumatic conveyors to specialized powder and grain conveying solutions, pneumatic systems help businesses improve productivity, reduce operational costs, and maintain high-quality standards. Choosing the right pneumatic conveying system ensures smooth production and long-term efficiency. For expert guidance and a customized quote, Contact Us today.
Pressure conveying pushes materials through pipelines using positive air pressure, while vacuum conveying pulls materials using negative pressure.
Dilute phase conveying uses higher air velocity and lower material concentration, while dense phase conveying uses lower velocity and higher material concentration.
The right system depends on material properties, required capacity, conveying distance, pipeline layout, and operating conditions.
System design is affected by material characteristics, conveying capacity, distance, air velocity, pipeline size, pressure requirements, and plant layout.
Capacity is determined based on material properties, required throughput, conveying distance, pipeline size, and available air pressure or vacuum.
Yes, Pneumatic Conveying Systems can be designed for long-distance material transfer by selecting suitable conveying methods and system parameters.
Yes, suitable conveying conditions such as lower velocity and dense phase operation can help reduce impact and material degradation.
Yes, properly designed pneumatic conveying systems can improve energy efficiency by optimizing airflow, pressure, pipeline sizing, and operating conditions.
Maintenance requirements are generally manageable and include regular inspection of filters, pipelines, valves, feeders, blowers, and other operating components.
Yes, Pneumatic Conveying Systems can be configured according to material characteristics, capacity, conveying distance, automation needs, and industry requirements.
Designed & Developed by